Efficiency (AQA A Level Business): Exam Questions

Exam code: 7132

Syllabus Edition

First teaching 2026

First exams 2028

2 hours15 questions
1
6 marks

Source B: Warburtons

Warburtons is the largest family-owned bakery business in the United Kingdom and in 2025 it entered its 150th year. It is still owned by the Warburton family, bakes in 13 bakeries and employs just over 5 000 people.

The year to 27 September 2025 was a record one. Revenue grew 3.9% to £769.9 million and the volume of products sold grew 4.2%. Operating profit rose 30%, from £33.3 million to £43.2 million, and profit before tax rose 33% to £42 million. During the year the company recruited more than 400 new employees, although after leavers the workforce grew by only 45. It also bought a former Rathbones bakery, which it expects to have running by September 2026.

Even after that jump in profit, Warburtons keeps only a few pence of every pound it takes. Bread is sold mainly through a handful of large supermarkets, which negotiate hard on price, so the company cannot pass higher costs on. Almost all of its improvement has to come from making bread more cheaply and wasting less of it.

That is difficult, because a standard loaf has a shelf life of five days and the business is judged on getting it onto the shelf fast. Bread that is rejected at the bakery, or returned unsold by a retailer, cannot be sold at all. Over the last four years both of those figures have been rising, and its bakeries differ widely in how much bread each employee produces.

Source: Warburtons annual results for the year to 27 September 2025

Appendix F: Output and employees at four Warburtons bakeries

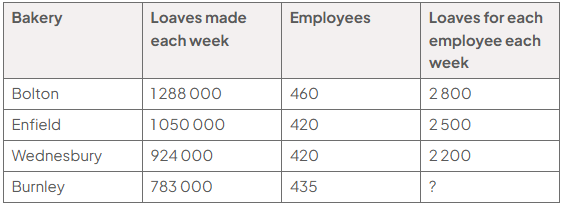
Table of weekly bakery output and employees: Bolton 1 288 000 loaves, 460 employees, 2 800 each; Enfield 1 050 000, 420, 2 500; Wednesbury 924 000, 420, 2 200; Burnley 783 000, 435, not provided.

All four bakeries use the same equipment and make the same products.

Source: Analyst
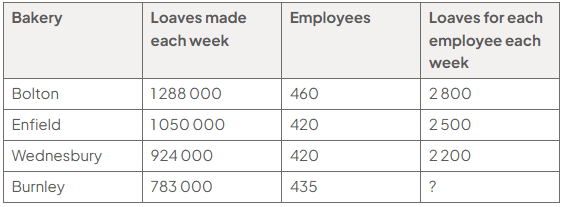
Analyse one way in which raising productivity at the Burnley bakery to the level of the Bolton bakery might affect Warburtons' profit.

2
6 marks

Source B: Aldermoor Precision Ltd

Aldermoor Precision Ltd machines metal components to order for aerospace and medical equipment makers. It has one workshop in Hampshire, 42 employees and a small number of large customers, each of whom sends drawings and expects parts made to within a few hundredths of a millimetre.

In the year to March 2025 it made 92 400 components, had revenue of £3 696 000 and an operating profit of £369 600. The operating margin was 10%, down from 14% three years earlier.

Nothing has gone obviously wrong. What has happened is that more components are being made twice. A part that is out of tolerance can sometimes be reworked, which uses machine time that was meant for the next job, and sometimes has to be scrapped, which loses the material as well. Both have been rising for two years, and because almost every job is made to a customer's drawing rather than held as inventory, a scrapped part usually means a late delivery too.

The managing director, Ruth Castellan, has two proposals on her desk. One is to buy a second computer-controlled machining centre, which would let the workshop take on more work. The other is to stop organising the workshop by type of machine — all the lathes together, all the mills together — and instead group machines into cells, each cell making a family of similar parts from start to finish, with the operators trained to run every machine in their cell.

The first costs nearly four times as much as the second. The second means the workshop does more with fewer people.

Source: Aldermoor Precision Ltd

Appendix G: Why components fail inspection at Aldermoor Precision Ltd

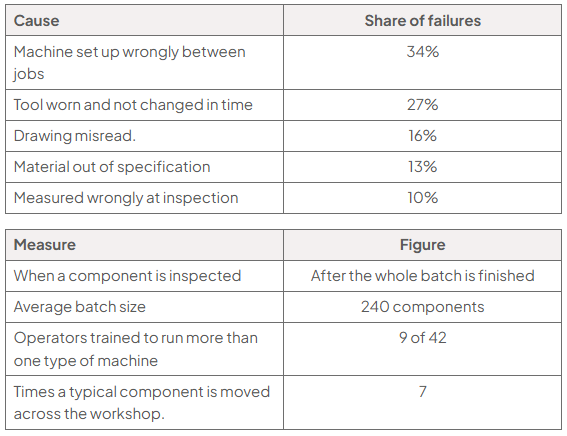
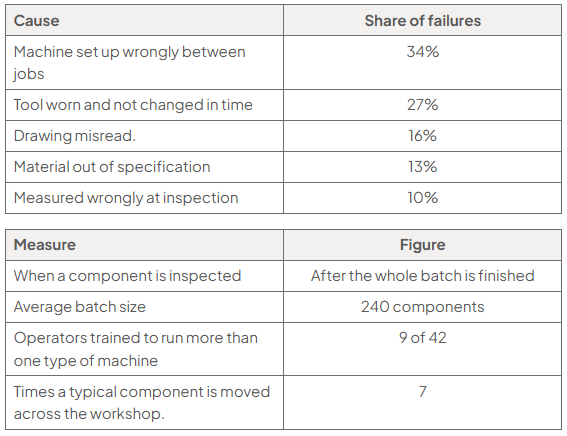
Table of failure causes and shares: wrong machine set-up 34%, worn tool 27%, misread drawing 16%, out-of-specification material 13%, wrong inspection measurement 10%. Measures: inspection after batch; average batch 240; 9 of 42 operators run multiple machine types; moved 7 times.

Source: Aldermoor Precision Ltd

Analyse one way in which moving a component across the workshop seven times might affect Aldermoor Precision Ltd's efficiency.

3
6 marks

Source B: Nissan Sunderland

Nissan's plant in Sunderland is the largest car factory in the United Kingdom. It opened in 1986, has built more than 11 million vehicles, and for years has turned out roughly one car every two minutes. It employs about 6 000 people directly, and tens of thousands more work for the suppliers around it.

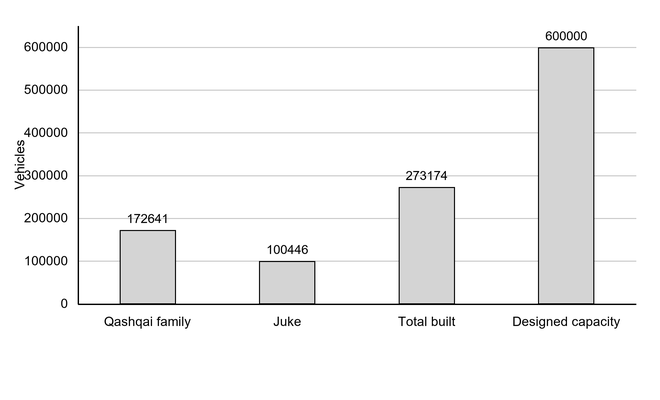
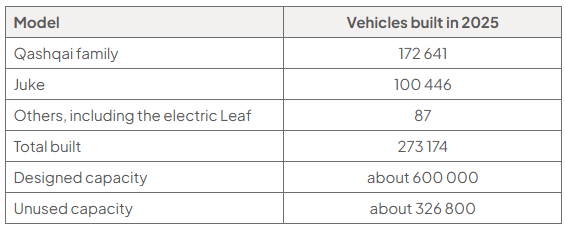
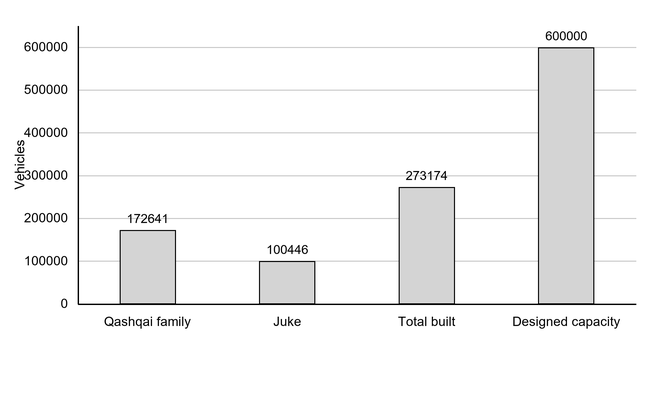
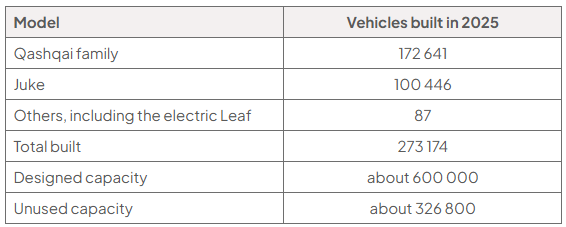
In 2025 the plant built 273 174 vehicles: 172 641 of the Qashqai family and 100 446 Jukes, plus a small number of others. It also makes the latest electric Leaf, and from 2027 it will add a battery-electric Juke, followed by a battery-electric Qashqai.

The difficulty is not whether Sunderland can build cars well. It is how many it is building. The plant was designed to make around 600 000 vehicles a year, so it is running at well under half of what it could do. Every year the factory carries the cost of a building, the machinery inside it and the people who keep it running, whether it makes 273 000 cars or 600 000.

In May 2026 Nissan announced it would bring production together onto a single line rather than running two, which would mean a smaller factory making much better use of itself. The alternative was to keep both lines and try to win enough new models to fill them.

Source: Nissan Sunderland Plant and Nissan Europe announcements, 2025 to 2026

Appendix F: What Sunderland built against what it could build

Bar chart of Nissan Sunderland vehicle numbers, showing Qashqai family 172 641, Juke 100 446, total built 273 174 and designed capacity 600 000. Vertical axis: vehicles, 0 to 600 000.
Table of Nissan Sunderland vehicles built in 2025: Qashqai family 172 641; Juke 100 446; others 87; total 273 174; designed capacity about 600 000; unused capacity about 326 800.

Source: Nissan

Analyse one way in which running at about 46% of capacity might affect Nissan Sunderland's unit costs.

4
6 marks

Source B: Toyota Manufacturing UK

Toyota Manufacturing UK builds the Corolla Hatchback and Corolla Touring Sports at Burnaston in Derbyshire, and the engines that go into them at Deeside in north Wales. Together the two plants employ about 3 000 people. Burnaston began building cars in December 1992 and built its five millionth British car, a Corolla, in October 2024.

A finished car leaves the Burnaston line roughly every 90 seconds, and about 150 000 cars a year are built there. Around 85% are exported, most of them to Europe, so the plant is judged against Toyota's other factories and has to win its work rather than be handed it.

Burnaston is run on the Toyota Production System. Anyone on the line may stop it by pulling a cord if something is not right, and it does not restart until the problem is understood. Teams meet in short standing huddles at the start of each shift, and improvements suggested by the people doing the job are expected rather than hoped for.

That makes the plant unusual in how much it measures. It records the time taken at every station, the number of cars that come off the line needing no further work, the defects found for each vehicle and the cost of putting them right. None of these figures are kept quiet: they are written up on boards the whole shift can see.

The pressure now is cost. European plants with newer lines and lower wages build the same model, and Burnaston has been asked to find a further saving on every car without spending heavily on new equipment.

Source: Toyota Manufacturing UK and Toyota Motor Europe

Appendix F: What Burnaston measures

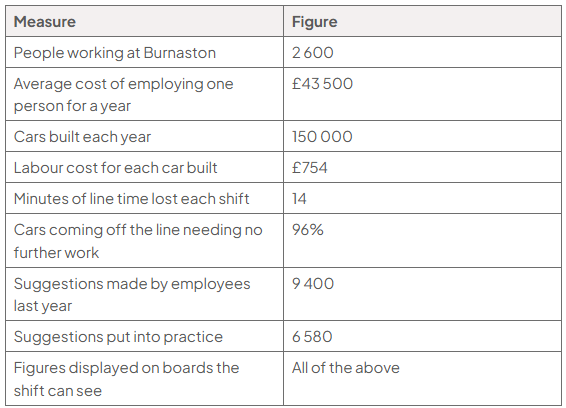
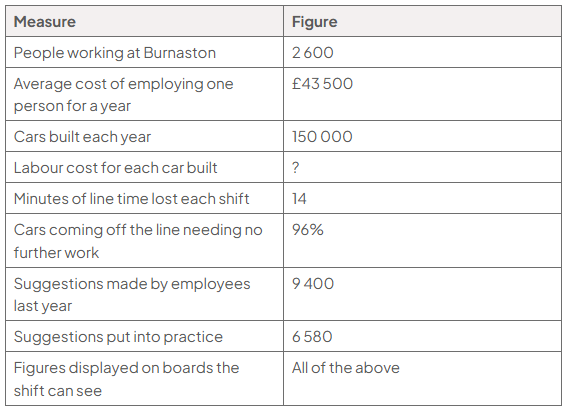
Burnaston measures table: 2 600 employees; £43 500 annual cost per employee; 150 000 cars yearly; labour cost per car £754; 14 minutes lost per shift; 96% need no further work; 9 400 suggestions, 6 580 implemented; all figures displayed.

Source: Analyst

Analyse one way in which putting 6 580 employee suggestions into practice might affect efficiency at Burnaston.

5
6 marks

Source B: 2 Sisters Food Group

2 Sisters Food Group is one of Britain's largest food manufacturers. It supplies roughly a third of the poultry eaten in the country, also makes ready meals and bakery products, employs around 13 500 people across about twenty United Kingdom sites, and is privately owned as part of Boparan Holdings. In the year to 27 July 2024 turnover was £3.05 billion, up 0.5%, with a profit before tax of £35.5 million.

Poultry is one of the most heavily checked things made in Britain. Temperature is recorded continuously, every batch is inspected, and the sites are audited by their own quality teams, by the supermarket customers who buy from them, by the regulator and by independent certification bodies. Over a year that comes to more than a thousand separate audits.

Everything about the operation is measured because almost nothing about it can be put right later. A bird that is wrong cannot be reworked; it is taken out. A line that stops costs a shift's output, and a site stopped for a day costs hundreds of thousands of pounds. Sixty-eight per cent of sales go to four supermarket customers, and each of them can audit a site at five days' notice.

That leaves two numbers in tension. The sites run close to flat out and want to keep running, and the same sites have to be able to prove what happened to every bird. Stopping the line protects the second and costs the first.

The question in front of the operations board is what would improve what the sites can prove, rather than only what they produce.

Source: Boparan Holdings Limited annual results for the year ended 27 July 2024

Appendix F: What a poultry site measures

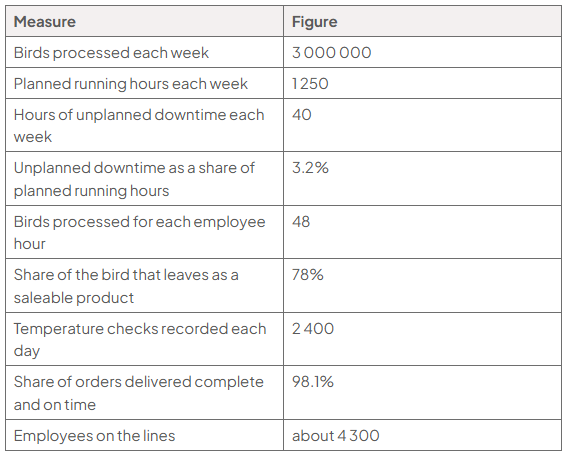
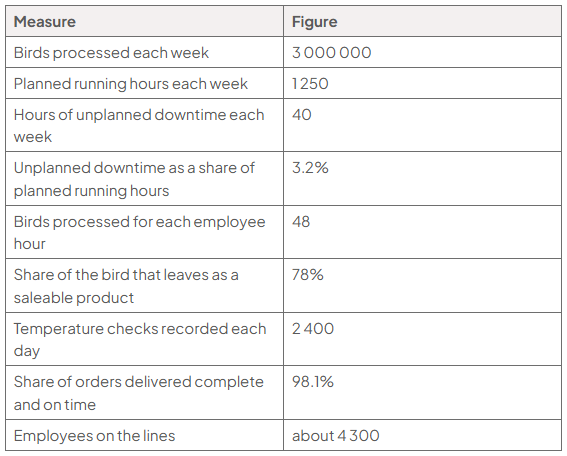
Two-column table, “What a poultry site measures”, listing operating, quality and workforce measures. It shows 40 hours of unplanned downtime against 1,250 planned hours; unplanned downtime is 3.2% of planned hours.

Figures cover the sites in this report, not the whole group

Source: Analyst

Analyse one way in which 40 hours of unplanned downtime a week might affect 2 Sisters Food Group's costs.

6
6 marks

Source B: Marchwood Precision Ltd

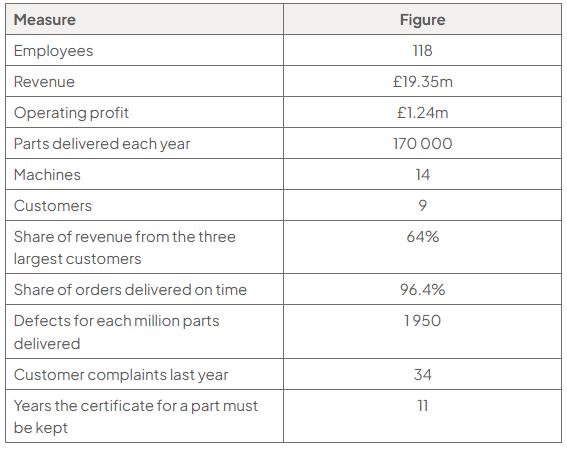
Marchwood Precision Ltd machines aluminium parts for aerospace customers from a single factory near Bristol. It delivers about 170 000 parts a year to nine customers, three of whom provide 64% of revenue. Revenue in the year to March 2025 was £19.35 million and operating profit £1.24 million. It employs 118 people and runs fourteen machines on two shifts.

Aerospace work is sold on paperwork as much as on metal. Every part leaves with a certificate saying what it was made from and who machined it, and those records have to be kept for eleven years. A part that is wrong cannot be quietly used up somewhere else; it is scrapped or sent back through the shop to be reworked.

Last year 2.1% of parts were scrapped and 1.6% were reworked, which cost £412 000 and £268 000. A further £94 000 went on warranty claims. Six inspectors check every part, but they check it after machining is finished, so a mistake made in the first minute of a cut is found an hour later when nothing can be done about it.

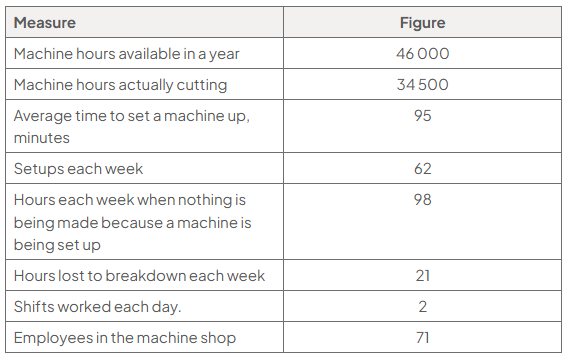
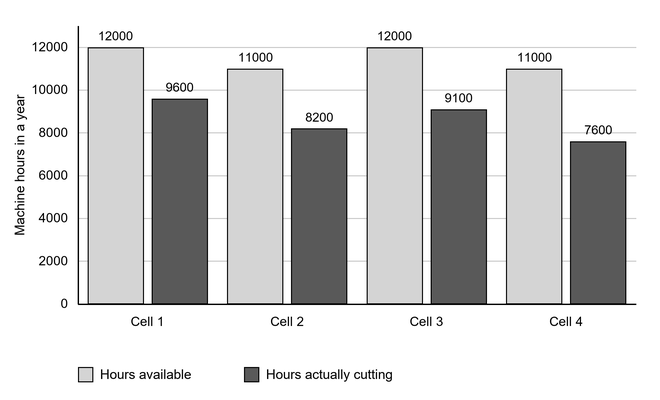
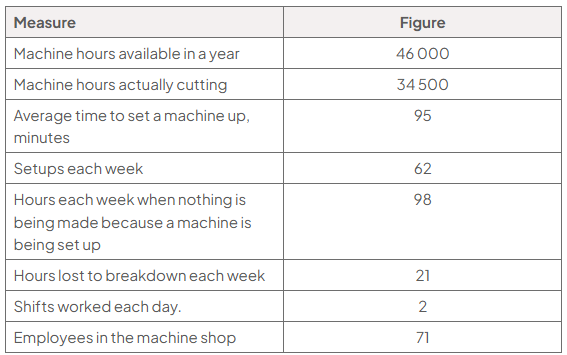
The machines themselves are not the constraint. They could cut for 46 000 hours a year and actually cut for 34 500. Most of the gap is setting up: 62 setups a week at an average of 95 minutes each, which is about 98 hours a week when nothing is being made.

The board has agreed that quality has to improve before the next contract review, and is choosing between two ways of doing it.

Source: Marchwood Precision Ltd

Appendix G: How the machine shop runs

Machine hours in a year

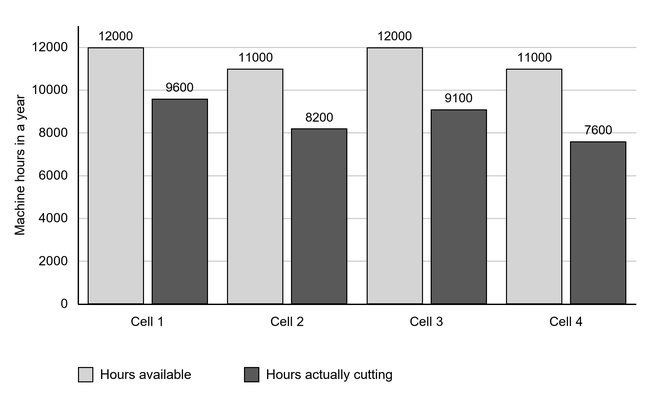
Bar chart of annual machine hours, showing actual cutting below available capacity in every cell: Cell 1, 12,000 versus 9,600; Cell 2, 11,000 versus 8,200; Cell 3, 12,000 versus 9,100; Cell 4, 11,000 versus 7,600.
Table of machine-shop measures: 46,000 hours available and 34,500 cutting; 95-minute setups, 62 setups and 98 setup hours weekly; 21 breakdown hours, two daily shifts and 71 employees.

Source: Analyst

Analyse one way in which losing 98 hours a week to setting machines up might affect Marchwood Precision Ltd.

7
6 marks

Source A: Dalmuir Shipworks Ltd

Dalmuir Shipworks Ltd repairs ships and offshore vessels in three dry berths on the Clyde. The yard has been working for ninety-six years, employs 290 people and had revenue of £42.8 million in the year to March 2025, with an operating profit of £2.3 million.

Seventy-eight per cent of the workforce is in the union, which appoints six safety representatives. They stopped work twenty-three times last year. There is a written safety procedure signed off with the union, nine reportable injuries were recorded, and 435 working days were lost to injury.

Because the yard employs more than 250 people it has to publish its gender pay gap, and the figures are uncomfortable reading. Thirty-two of the 290 employees are women, which is 11%. The median hourly rate for men is £19.20 and for women £16.32. Women make up 24% of the lowest-paid quarter of employees and 2% of the highest-paid quarter. None of the fourteen supervisors is a woman, and men are far more likely than women to receive a bonus.

The commercial problem is different and just as hard. The three berths are only full three days in four. A third of the yard's revenue comes from work that arrives at short notice, which is exactly the work that needs an empty berth, and the only ways of filling the gaps are to work through the night or to stop taking short-notice jobs at all.

The board is reviewing both the pay figures and the berths this spring.

Source: Dalmuir Shipworks Ltd

Appendix C: How the yard works, and what lost time costs

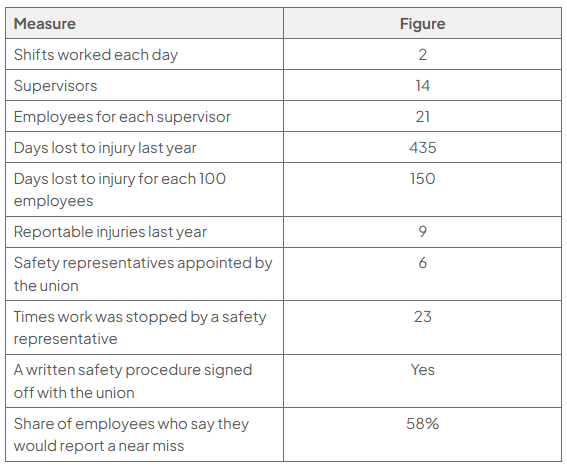
Two-column table headed “Measure” and “Figure”, listing yard staffing, injury and safety data: two shifts, 14 supervisors, 435 days lost, nine injuries, six safety representatives, 23 stoppages, and 58% near-miss reporting.

Source: Analyst

Analyse one way in which work being stopped twenty-three times last year by a safety representative might affect Dalmuir Shipworks Ltd's efficiency.

1
9 marks

Source A: SHEIN

SHEIN is an online fashion retailer. It has nearly 10 000 employees, sells in over 150 countries and operates in over 20 languages.

SHEIN's annual revenue target for 2025 is $58.5 billion, up from $22.7 billion in 2022. That would exceed the existing combined sales of its main competitors, H&M and Zara.

The average price of an item sold by SHEIN is just £7.90. The company's website has over 600 000 items on sale. It adds 6 000 new items each day.

SHEIN has a lean production model. It only produces 100 to 200 pieces of any item when launched and responds with increased production only if demand justifies it. The company uses computer models to try and estimate future sales accurately and match production to demand more closely than its competitors. Through its on-demand production, SHEIN is able to consistently limit the amount of excess inventory to a level that is much lower than traditional retailers.

The company supports its suppliers with training and investment in advanced technology. SHEIN ships orders to its customers directly, mostly from one huge warehouse near Guangzhou in China. This means that deliveries to customers around the world are slower than those of some competitors who have warehouses in different countries.

The fast fashion business model that SHEIN adopts has been widely criticised. It has been suggested that 8% of global carbon emissions are produced by the fashion industry. Fast fashion businesses are also criticised for encouraging consumers to replace, rather than repair or reuse clothing. Fast fashion allows customers to buy cheap products which they then discard, before quickly buying something new. There have also been criticisms of conditions in some of SHEIN's suppliers' factories in China.

SHEIN has now decided to focus more on environmental sustainability. It states, "Our operations are guided by a sustainability mindset tackling waste and circularity at every stage". The company aims to optimise the efficiency of its processes to conserve water, energy and raw materials while minimising waste. In September 2022, as part of its sustainability approach, SHEIN committed to reducing absolute (total) greenhouse gas emissions by 25% by 2030, when those of the industry are predicted to rise by 45% by 2030.

SHEIN has strict quality standards. Its approach includes a quality-check process where products are examined when they arrive at the warehouse. Factors tested include tear-strength and whether the colour of an item will fade when washed. Departments within the business are treated as if they are customers as part of its quality assurance approach.

SHEIN's values for employees include being good team-players who work well in a collaborative environment.

If SHEIN was seeking to launch a new range of clothing in 2026, it might consider two new suppliers: Xpress and Reliont. Appendix A shows information on these suppliers. The expected orders for the product in the first year would total 2.4 million units.

Source: Shein, 2024

Assess the impact of SHEIN using lean production on its market share.

2
9 marks

Source B: Warburtons

Warburtons is the largest family-owned bakery business in the United Kingdom and in 2025 it entered its 150th year. It is still owned by the Warburton family, bakes in 13 bakeries and employs just over 5 000 people.

The year to 27 September 2025 was a record one. Revenue grew 3.9% to £769.9 million and the volume of products sold grew 4.2%. Operating profit rose 30%, from £33.3 million to £43.2 million, and profit before tax rose 33% to £42 million. During the year the company recruited more than 400 new employees, although after leavers the workforce grew by only 45. It also bought a former Rathbones bakery, which it expects to have running by September 2026.

Even after that jump in profit, Warburtons keeps only a few pence of every pound it takes. Bread is sold mainly through a handful of large supermarkets, which negotiate hard on price, so the company cannot pass higher costs on. Almost all of its improvement has to come from making bread more cheaply and wasting less of it.

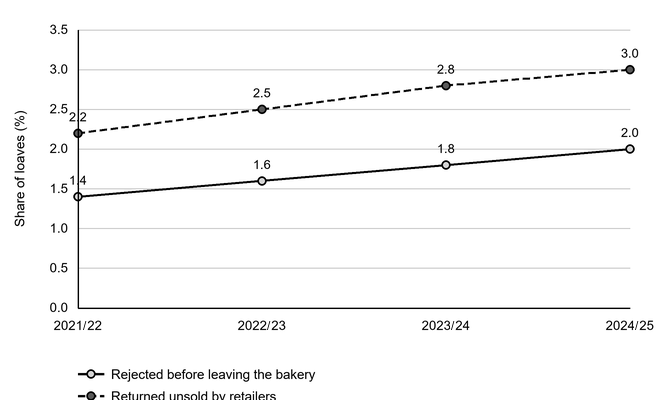
That is difficult, because a standard loaf has a shelf life of five days and the business is judged on getting it onto the shelf fast. Bread that is rejected at the bakery, or returned unsold by a retailer, cannot be sold at all. Over the last four years both of those figures have been rising, and its bakeries differ widely in how much bread each employee produces.

Source: Warburtons annual results for the year to 27 September 2025

Appendix F: Output and employees at four Warburtons bakeries

Table comparing weekly output, employees and loaves per employee: Bolton 1 288 000, 460, 2 800; Enfield 1 050 000, 420, 2 500; Wednesbury 924 000, 420, 2 200; Burnley 783 000, 435, not provided.

All four bakeries use the same equipment and make the same products.

Source: Analyst

Appendix G: Quality and waste at Warburtons

Line chart of Warburtons’ wasted loaves as a share of total, showing both measures rising from 2021/22 to 2024/25: bakery rejects 1.4% to 2.0%, and retailer returns 2.2% to 3.0%.
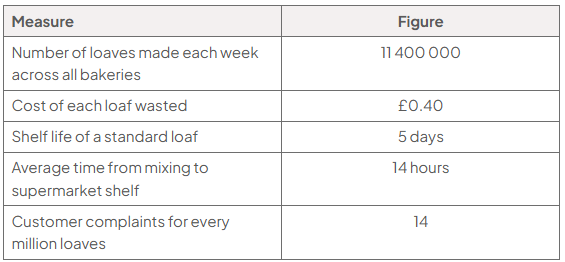
Table of Warburtons bakery measures: 11 400 000 loaves made weekly; £0.40 cost per wasted loaf; five-day shelf life; 14 hours from mixing to supermarket shelf; 14 complaints per million loaves.

Source: Analyst

Assess whether improving efficiency is the most important way for Warburtons to raise its operating profit.

3
9 marks

Source B: Nissan Sunderland

Nissan's plant in Sunderland is the largest car factory in the United Kingdom. It opened in 1986, has built more than 11 million vehicles, and for years has turned out roughly one car every two minutes. It employs about 6 000 people directly, and tens of thousands more work for the suppliers around it.

In 2025 the plant built 273 174 vehicles: 172 641 of the Qashqai family and 100 446 Jukes, plus a small number of others. It also makes the latest electric Leaf, and from 2027 it will add a battery-electric Juke, followed by a battery-electric Qashqai.

The difficulty is not whether Sunderland can build cars well. It is how many it is building. The plant was designed to make around 600 000 vehicles a year, so it is running at well under half of what it could do. Every year the factory carries the cost of a building, the machinery inside it and the people who keep it running, whether it makes 273 000 cars or 600 000.

In May 2026 Nissan announced it would bring production together onto a single line rather than running two, which would mean a smaller factory making much better use of itself. The alternative was to keep both lines and try to win enough new models to fill them.

Source: Nissan Sunderland Plant and Nissan Europe announcements, 2025 to 2026

Appendix F: What Sunderland built against what it could build

Bar chart of Nissan Sunderland vehicle numbers: Qashqai family 172,641, Juke 100,446, total built 273,174, compared with designed capacity 600,000. Vertical axis shows vehicles from 0 to 600,000.
Table of Nissan Sunderland vehicles built in 2025: Qashqai family 172,641; Juke 100,446; others including electric Leaf 87; total 273,174. Designed capacity is about 600,000, leaving about 326,800 unused.

Source: Nissan

Appendix G: Cost and quality at Sunderland

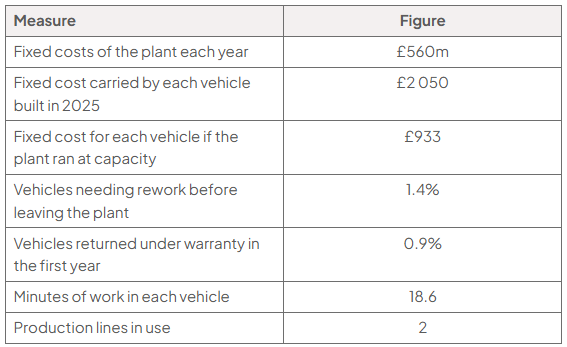
Table of cost and quality measures at Sunderland: annual fixed costs £560m; fixed cost per 2025 vehicle £2,050, or £933 at capacity; rework 1.4%; warranty returns 0.9%; 18.6 minutes’ work per vehicle; two production lines.

Source: Analyst

Assess whether improving capacity utilisation is the most important way for Nissan to reduce costs at Sunderland.

4
9 marks

Source B: 2 Sisters Food Group

2 Sisters Food Group is one of Britain's largest food manufacturers. It supplies roughly a third of the poultry eaten in the country, also makes ready meals and bakery products, employs around 13 500 people across about twenty United Kingdom sites, and is privately owned as part of Boparan Holdings. In the year to 27 July 2024 turnover was £3.05 billion, up 0.5%, with a profit before tax of £35.5 million.

Poultry is one of the most heavily checked things made in Britain. Temperature is recorded continuously, every batch is inspected, and the sites are audited by their own quality teams, by the supermarket customers who buy from them, by the regulator and by independent certification bodies. Over a year that comes to more than a thousand separate audits.

Everything about the operation is measured because almost nothing about it can be put right later. A bird that is wrong cannot be reworked; it is taken out. A line that stops costs a shift's output, and a site stopped for a day costs hundreds of thousands of pounds. Sixty-eight per cent of sales go to four supermarket customers, and each of them can audit a site at five days' notice.

That leaves two numbers in tension. The sites run close to flat out and want to keep running, and the same sites have to be able to prove what happened to every bird. Stopping the line protects the second and costs the first.

The question in front of the operations board is what would improve what the sites can prove, rather than only what they produce.

Source: Boparan Holdings Limited annual results for the year ended 27 July 2024

Appendix E: 2 Sisters Food Group, published figures

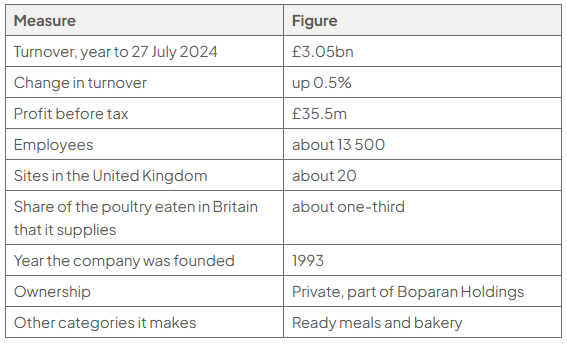
Table of 2 Sisters Food Group published figures: turnover in the year to 27 July 2024 £3.05bn, up 0.5%; profit before tax £35.5m; about 13 500 employees; about 20 sites in the United Kingdom; supplies about one-third of the poultry eaten in Britain; founded in 1993; privately owned, part of Boparan Holdings; also makes ready meals and bakery.

Source: Boparan Holdings Limited

Appendix F: What a poultry site measures

Two-column table of poultry-site measures: 3 000 000 birds/week; 1 250 planned hours; 40 unplanned downtime hours; downtime share 3.2%; 48 birds per employee hour; 78% saleable; 2 400 checks/day; 98.1% complete and on time; about 4 300 line employees.

Figures cover the sites in this report, not the whole group

Source: Analyst

Assess how efficiently 2 Sisters Food Group's poultry sites are running.

Calculate the capacity utilisation of the poultry sites, based on their planned running hours, to support your answer.

5
9 marks

Source B: Marchwood Precision Ltd

Marchwood Precision Ltd machines aluminium parts for aerospace customers from a single factory near Bristol. It delivers about 170 000 parts a year to nine customers, three of whom provide 64% of revenue. Revenue in the year to March 2025 was £19.35 million and operating profit £1.24 million. It employs 118 people and runs fourteen machines on two shifts.

Aerospace work is sold on paperwork as much as on metal. Every part leaves with a certificate saying what it was made from and who machined it, and those records have to be kept for eleven years. A part that is wrong cannot be quietly used up somewhere else; it is scrapped or sent back through the shop to be reworked.

Last year 2.1% of parts were scrapped and 1.6% were reworked, which cost £412 000 and £268 000. A further £94 000 went on warranty claims. Six inspectors check every part, but they check it after machining is finished, so a mistake made in the first minute of a cut is found an hour later when nothing can be done about it.

The machines themselves are not the constraint. They could cut for 46 000 hours a year and actually cut for 34 500. Most of the gap is setting up: 62 setups a week at an average of 95 minutes each, which is about 98 hours a week when nothing is being made.

The board has agreed that quality has to improve before the next contract review, and is choosing between two ways of doing it.

Source: Marchwood Precision Ltd

Appendix E: Marchwood Precision Ltd selected data, year to March 2025

Table of Marchwood Precision Ltd selected data: 118 employees; revenue £19.35m; operating profit £1.24m; 170 000 parts delivered each year; 14 machines; 9 customers; 64% of revenue from the three largest customers; 96.4% of orders delivered on time; 1 950 defects for each million parts delivered; 34 customer complaints last year; the certificate for a part must be kept for 11 years.

Source: Marchwood Precision Ltd

Appendix G: How the machine shop runs

Machine hours in a year

Bar chart of machine hours by cell: available versus actually cutting. Cell 1: 12 000 and 9 600; Cell 2: 11 000 and 8 200; Cell 3: 12 000 and 9 100; Cell 4: 11 000 and 7 600 hours.
Table headed “Measure” and “Figure”: 46 000 machine hours available yearly, 34 500 actually cutting; 95-minute average setup, 62 setups weekly and 98 weekly hours setting up; 21 breakdown hours weekly, two daily shifts and 71 shop employees.

Source: Analyst

Assess how efficiently Marchwood Precision Ltd uses its machines.

Calculate its capacity utilisation to support your answer.

1
15 marks

Source B: Aldermoor Precision Ltd

Aldermoor Precision Ltd machines metal components to order for aerospace and medical equipment makers. It has one workshop in Hampshire, 42 employees and a small number of large customers, each of whom sends drawings and expects parts made to within a few hundredths of a millimetre.

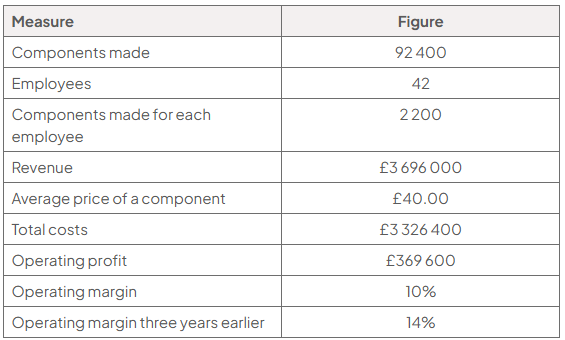
In the year to March 2025 it made 92 400 components, had revenue of £3 696 000 and an operating profit of £369 600. The operating margin was 10%, down from 14% three years earlier.

Nothing has gone obviously wrong. What has happened is that more components are being made twice. A part that is out of tolerance can sometimes be reworked, which uses machine time that was meant for the next job, and sometimes has to be scrapped, which loses the material as well. Both have been rising for two years, and because almost every job is made to a customer's drawing rather than held as inventory, a scrapped part usually means a late delivery too.

The managing director, Ruth Castellan, has two proposals on her desk. One is to buy a second computer-controlled machining centre, which would let the workshop take on more work. The other is to stop organising the workshop by type of machine — all the lathes together, all the mills together — and instead group machines into cells, each cell making a family of similar parts from start to finish, with the operators trained to run every machine in their cell.

The first costs nearly four times as much as the second. The second means the workshop does more with fewer people.

Source: Aldermoor Precision Ltd

Appendix E: Aldermoor Precision Ltd selected data, year to March 2025

Table of Aldermoor Precision Ltd data: 92,400 components, 42 employees, 2,200 per employee, revenue £3,696,000, average price £40, costs £3,326,400, profit £369,600, margin 10%, previously 14%.

Source: Aldermoor Precision Ltd

Appendix G: Why components fail inspection at Aldermoor Precision Ltd

Two tables: failure causes: wrong machine setup 34%, worn tool 27%, misread drawing 16%, faulty material 13%, inspection error 10%; measures: batch-end inspection, 240 components per batch, 9 of 42 operators multi-skilled, seven moves.

Source: Aldermoor Precision Ltd

Appendix H: Two ways of raising output at Aldermoor Precision Ltd

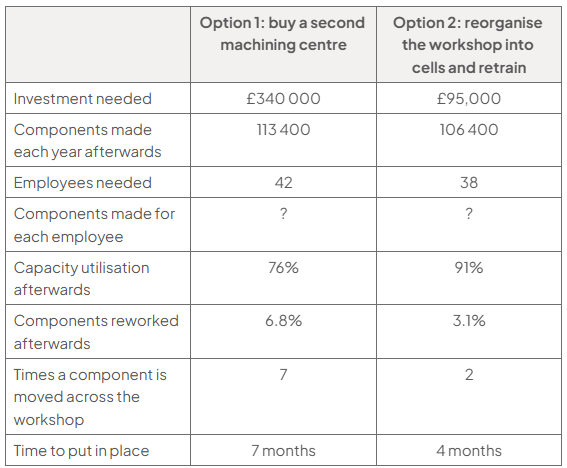
Comparison table: Option 1, second machining centre, versus Option 2, workshop cells and retraining. Data are investment, output, employees, capacity, reworked components, moves and time: £340,000/£95,000; 113,400/106,400; 42/38; 76%/91%; 6.8%/3.1%; 7/2; 7/4 months.

Source: Analyst

Aldermoor Precision Ltd is considering two ways of raising its output:

Option 1: buy a second machining centre

Option 2: reorganise the workshop into cells and retrain the operators

Evaluate both options and recommend which one Aldermoor Precision Ltd should choose.

Calculate the number of components each employee would make under Option 2 to support your answer.

2
15 marks

Source B: Toyota Manufacturing UK

Toyota Manufacturing UK builds the Corolla Hatchback and Corolla Touring Sports at Burnaston in Derbyshire, and the engines that go into them at Deeside in north Wales. Together the two plants employ about 3 000 people. Burnaston began building cars in December 1992 and built its five millionth British car, a Corolla, in October 2024.

A finished car leaves the Burnaston line roughly every 90 seconds, and about 150 000 cars a year are built there. Around 85% are exported, most of them to Europe, so the plant is judged against Toyota's other factories and has to win its work rather than be handed it.

Burnaston is run on the Toyota Production System. Anyone on the line may stop it by pulling a cord if something is not right, and it does not restart until the problem is understood. Teams meet in short standing huddles at the start of each shift, and improvements suggested by the people doing the job are expected rather than hoped for.

That makes the plant unusual in how much it measures. It records the time taken at every station, the number of cars that come off the line needing no further work, the defects found for each vehicle and the cost of putting them right. None of these figures are kept quiet: they are written up on boards the whole shift can see.

The pressure now is cost. European plants with newer lines and lower wages build the same model, and Burnaston has been asked to find a further saving on every car without spending heavily on new equipment.

Source: Toyota Manufacturing UK and Toyota Motor Europe

Appendix E: Toyota Manufacturing UK, published figures

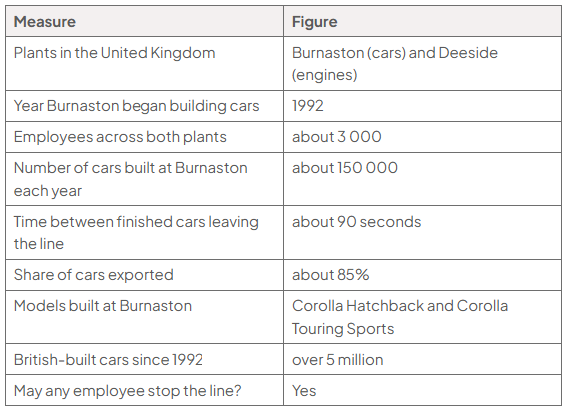
Table of Toyota Manufacturing UK published figures: plants in the United Kingdom, Burnaston (cars) and Deeside (engines); Burnaston began building cars in 1992; about 3 000 employees across both plants; about 150 000 cars built at Burnaston each year; about 90 seconds between finished cars leaving the line; about 85% of cars exported; models built at Burnaston, Corolla Hatchback and Corolla Touring Sports; over 5 million British-built cars since 1992; any employee may stop the line, yes.

Source: Toyota Manufacturing UK

Appendix F: What Burnaston measures

Table of Burnaston measures: 2 600 staff; £43 500 annual cost per employee; 150 000 cars yearly; labour cost per car not provided; 14 minutes lost per shift; 96% no rework; 9 400 suggestions, 6 580 implemented.

Source: Analyst

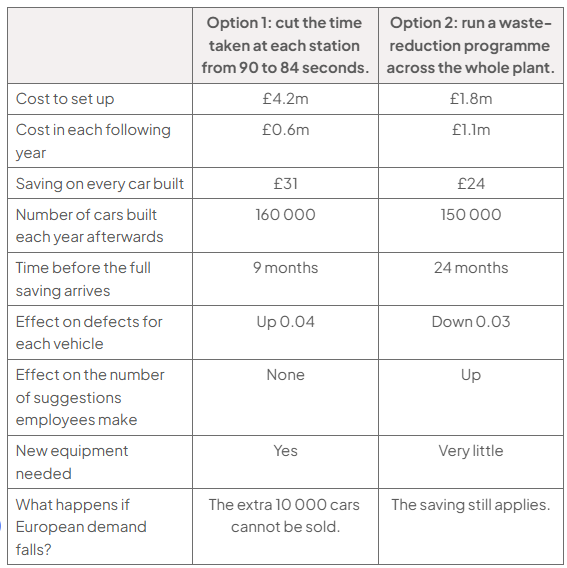
Appendix H: Two ways of lowering the cost of every car built at Burnaston

Table comparing Option 1 (90 to 84 seconds per station) with Option 2 (plant-wide waste reduction): setup £4.2m/£1.8m; annual £0.6m/£1.1m; saving per car £31/£24; output 160 000/150 000; full saving in 9/24 months; defects up 0.04/down 0.03; suggestions none/up; equipment yes/very little; demand fall: 10 000 unsold/saving remains.

Source: Analyst

Toyota Manufacturing UK is considering two ways of lowering the cost of every car built at Burnaston:

Option 1: cut the time taken at each station from 90 to 84 seconds

Option 2: run a waste-reduction programme across the whole plant

Evaluate both options and recommend which one Toyota Manufacturing UK should choose.

Calculate the labour cost for each car built at Burnaston to support your answer.

3
15 marks

Source A: Dalmuir Shipworks Ltd

Dalmuir Shipworks Ltd repairs ships and offshore vessels in three dry berths on the Clyde. The yard has been working for ninety-six years, employs 290 people and had revenue of £42.8 million in the year to March 2025, with an operating profit of £2.3 million.

Seventy-eight per cent of the workforce is in the union, which appoints six safety representatives. They stopped work twenty-three times last year. There is a written safety procedure signed off with the union, nine reportable injuries were recorded, and 435 working days were lost to injury.

Because the yard employs more than 250 people it has to publish its gender pay gap, and the figures are uncomfortable reading. Thirty-two of the 290 employees are women, which is 11%. The median hourly rate for men is £19.20 and for women £16.32. Women make up 24% of the lowest-paid quarter of employees and 2% of the highest-paid quarter. None of the fourteen supervisors is a woman, and men are far more likely than women to receive a bonus.

The commercial problem is different and just as hard. The three berths are only full three days in four. A third of the yard's revenue comes from work that arrives at short notice, which is exactly the work that needs an empty berth, and the only ways of filling the gaps are to work through the night or to stop taking short-notice jobs at all.

The board is reviewing both the pay figures and the berths this spring.

Source: Dalmuir Shipworks Ltd

Appendix C: How the yard works, and what lost time costs

Table of how the yard works: 2 shifts worked each day; 14 supervisors; 21 employees for each supervisor; 435 days lost to injury last year; 150 days lost to injury for each 100 employees; 9 reportable injuries last year; 6 safety representatives appointed by the union; work was stopped 23 times by a safety representative; a written safety procedure has been signed off with the union; 58% of employees say they would report a near miss.

Source: Analyst

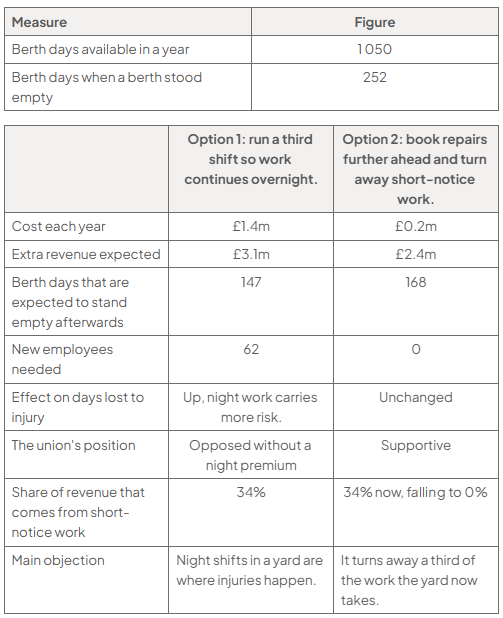
Appendix D: Two ways of getting more work through three berths

Three berths, each available 350 days a year

Tables show 1 050 annual berth-days, 252 empty. Option 1: £1.4m cost, £3.1m revenue, 147 empty days, 62 staff; injury risk rises and the union opposes it. Option 2: £0.2m, £2.4m, 168 empty days, no staff; injury unchanged, union supportive.

Source: Analyst

Dalmuir Shipworks Ltd is considering two ways of getting more work through its three berths:

Option 1: run a third shift so work continues overnight

Option 2: book repairs further ahead and turn away short-notice work

Evaluate both options and recommend which one Dalmuir Shipworks Ltd should choose.

Calculate Dalmuir Shipworks Ltd's current capacity utilisation, in berth days, to support your answer.